
Sprocket Manufacturer Guide: Types, Materials, Teeth and Heat Treatment
 ·
Updated October 10, 2026
·
22 min read
A sprocket is a toothed wheel, and it looks easy to buy: give the supplier a tooth count and a bore, and a price comes back. The trouble is that three of the four things that decide whether it works are not on that list. The pitch has to match the chain exactly, and the American and European chain systems do not label the same chain the same way. The teeth have to be hard enough for the rollers that will run on them, and "steel" does not say how hard. And the bore is the one feature that cannot be corrected later — which is why the bushing system on the back of the sprocket is often worth more than the price difference between two quotes. This guide covers which sprocket type your drive needs, how pitch and tooth count decide the ratio, what the materials and heat treatments actually buy, where the bore and keyway money goes, what the standards on a drawing do and do not cover, and why replacing a chain without its sprocket is the most expensive saving in power transmission.
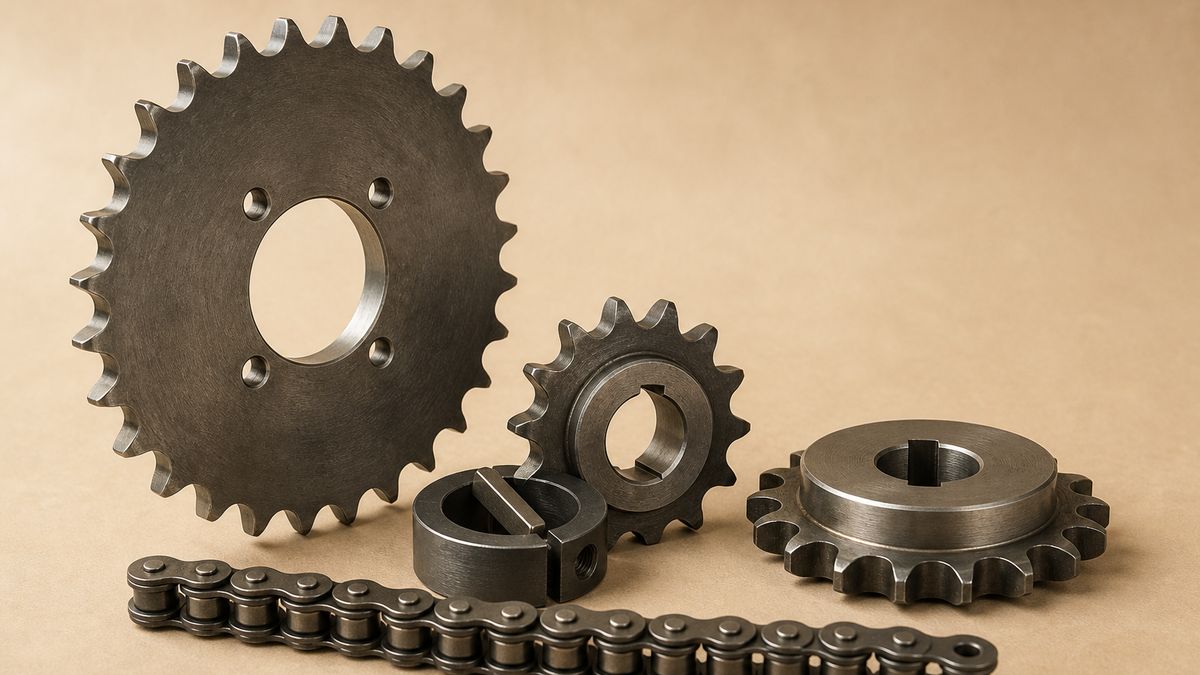
What Each Choice Actually Buys You
| If your situation is | The choice that follows | Why it is the right trade |
|---|---|---|
| The shaft is fixed and the sprocket is bought by size | Taper lock or QD bushed sprocket | The bushing carries the bore, so changing the shaft fit later means a new bushing instead of a new sprocket |
| Small driver, high speed, and the drive wears out at one end | Hardened teeth on the small sprocket | Fewer teeth are in mesh at the driver, so that is the sprocket that wears first — and hardening is cheap on a small part |
| Washdown, food or corrosive service | Stainless steel | A rusted sprocket is a worn sprocket, and the chain has to match the material or the pair corrodes together |
| Quiet running, light load, no lubrication wanted | Engineered plastic | Plastic sprockets run quietly and need no oil, but they carry far less load and the chain has to suit them |
What Is a Sprocket, and What Actually Decides Its Price?
A sprocket is a wheel with shaped teeth that engage the rollers of a chain, so that turning one shaft turns another at a set ratio. It is the oldest way of transmitting power mechanically and it is still the cheapest for many jobs, because a chain drive tolerates misalignment and shock that a gear drive will not.
The price of a sprocket is set by four things, and only one of them is on the drawing most buyers send:
- Pitch and tooth count
- The pitch is the spacing of the chain it has to run with, and the tooth count sets the ratio. Both come from the drive design rather than from the sprocket, which is why a sprocket ordered without them is a guess. A sprocket is not a stock item once the pitch and tooth count are unusual, and unusual tooth counts are cut rather than stamped.
- The material and its heat treatment
- Two sprockets of the same size and the same steel can differ by several times in life depending on whether the teeth were hardened and how deep the hardness goes. This is the single largest quality difference between a cheap quote and a careful one, and it is invisible in a photograph.
- How the teeth are made
- A tooth profile can be cut, milled, or formed, and the profile itself has to suit the chain. A sprocket whose teeth were formed from a stamping is fine for a light drive and wrong for a heavily loaded one, because the tooth geometry is less exact.
- The bore, keyway and mounting
- This is where most of the argument happens, because a bore cannot be reduced and a keyway cannot be moved. Whether the sprocket is a plain bore, a finished bore with a keyway, or a bushed design decides how much of your future is locked into this purchase.
The habit worth building is to treat the sprocket as half of a pair rather than as a part. A chain and its sprockets wear against each other, so the specification that matters is the pair: a given pitch, a given roller size, a given tooth profile and a comparable hardness on both sides. If you are buying power-transmission parts from China for the first time, the same logic of matching a component to the system it runs in is written up for the plastic gears in a sprocket, where the module and the mating part decide the specification in exactly the same way.
Which Sprocket Type Do You Actually Need?
Two separate questions get answered at once when a buyer says "sprocket". The first is what the sprocket does in the drive, which decides its shape. The second is how it attaches to the shaft, which decides its bore. Sorting them apart prevents the most common ordering mistake, which is choosing a mounting style for the wrong reason.
What the sprocket does. A driver sprocket sits on the input shaft and is usually the smaller of the two. A driven sprocket sits on the output shaft and is usually larger. An idler or tensioner sprocket takes up slack and does not transmit power, so it can often be made in a lighter material with fewer teeth engaged. A double or triple strand sprocket carries two or three chains side by side on the same hub, which is how a heavy load is spread without going to a bigger pitch.
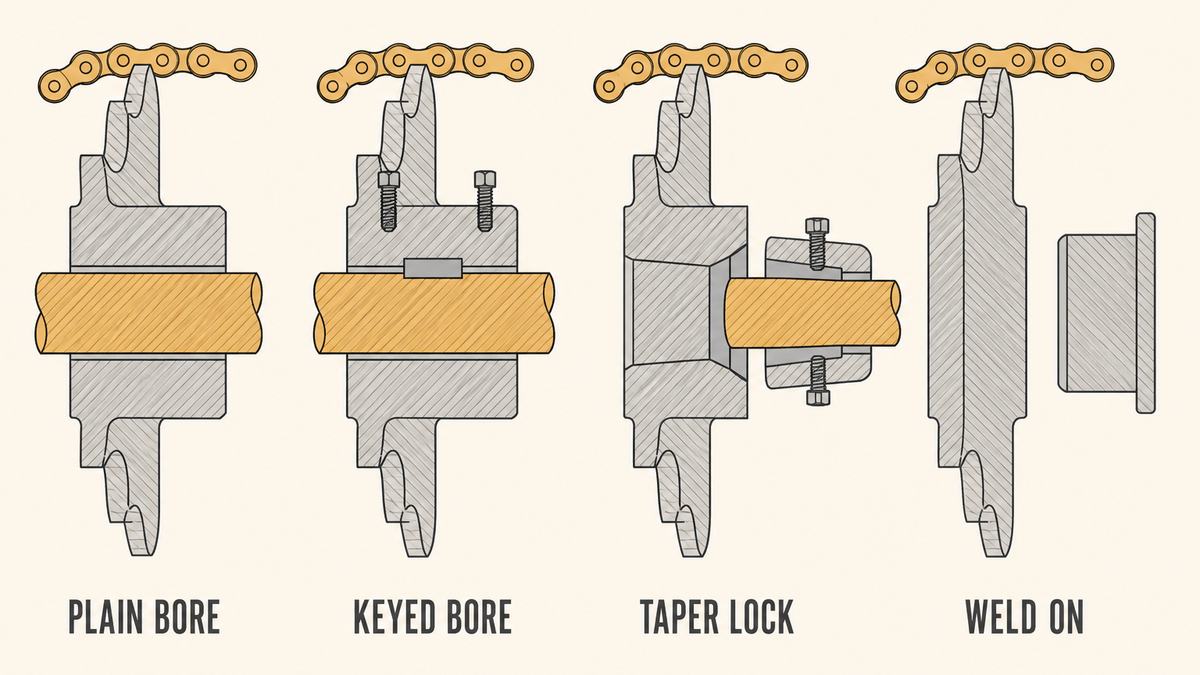
How it attaches to the shaft. This is the choice that follows you for years, because a bore cannot be shrunk:
- Plain bore. A hole with nothing else. Cheap, and only right if you will machine it yourself or if the shaft is exactly that size. Once it is bored out it cannot go back.
- Finished bore with a keyway. Bored and keyed to a named shaft size, usually with set screws. This is the normal industrial choice for a fixed shaft size, and it is a finished product rather than a blank.
- Taper lock or QD bushing. The sprocket has a tapered or flanged bore and a separate bushing grips the shaft. This is the flexible answer: change the shaft size and you change the bushing, not the sprocket. For anything you expect to maintain, it is usually the cheapest decision over the life of the drive.
- Weld-on or plate sprocket. A sprocket with no bore at all, welded or bolted onto a hub you already have. This is how odd shapes and very large diameters are handled without paying for a custom casting.
Pitch, Tooth Count and the Ratio That Decides Your Speed
Pitch is the distance from one chain pin to the next, and it is the number that has to match. A sprocket cut for one pitch will not run a chain of another, no matter how close the sizes look side by side. This is where the numbering systems cause trouble, because the American and the ISO or European systems describe similar chains but do not label them the same way.
The practical rule is to stop matching by the number on the chain and start matching by three dimensions: the pitch, the roller diameter, and the tooth count. Those three describe the joint between the chain and the sprocket, and they are the only things that decide whether the pair meshes at all. A part number is a shorthand that only works inside one system — and the standard that governs the American family of precision power transmission roller chains and their sprocket teeth is published by the American Society of Mechanical Engineers as ANSI/ASME B29.1, while other regions work to their own national and international equivalents.
The ratio comes from the teeth, not from the size. Dividing the driven tooth count by the driver tooth count gives you the speed reduction, and the same ratio can be built from many combinations — a large driver and a very large driven sprocket, or a small driver and a moderately large driven one. The choice between those combinations is not free:
- Small driver sprockets wear faster. With few teeth, each link has to flex through a larger angle as it enters and leaves the sprocket, and fewer rollers share the load. The driver is almost always the first part of a drive to fail.
- Large driven sprockets cost more in metal. Diameter grows quickly with tooth count, so a drive that needs a big reduction is often better built as two stages than as one enormous wheel.
- The pair has to fit the space you have. Ratio and center distance are set together, because the amount of chain wrapped around the smaller sprocket decides how much load each tooth carries. Too short a center distance means too few teeth in mesh, which is a wear problem rather than a strength problem.
None of this is the sprocket supplier's decision, and this is the point most buyers miss. A supplier can cut any tooth count you ask for; only you know what ratio the machine needs. Sending a drawing with a pitch, a tooth count and a bore, and saying nothing about the drive, leaves the supplier to make your engineering decision silently. The same boundary between what a fabricator can make and what only the buyer can decide shows up on a design for manufacturing review, and a sprocket ordered without one is a sprocket ordered on a guess.
Materials: Carbon Steel, Stainless, Cast Iron and Engineering Plastic
The material is chosen by the load, the environment and how long you want the drive to last. Four families cover almost everything you will be quoted.
- Carbon steel
- The default, and the material that most sprockets are cut from. It is strong, cheap and takes a heat treatment well, which is why the quality of a carbon steel sprocket is really a question about its hardening rather than about the metal. Steel bar for this kind of machining is bought to a published material specification — for hot-wrought carbon and alloy bars the usual reference is ASTM A29/A29M, and for cold-finished bar it is ASTM A108. Asking which of those the bar was bought to is a more useful question than asking whether the steel is "good".
- Stainless steel
- For washdown, food, marine and chemical environments. Two cautions. Stainless is softer than hardened carbon steel, so a stainless drive usually wears faster unless the load is modest. And a stainless sprocket on a plain steel chain corrodes the chain, so the pair has to be chosen together rather than part by part.
- Cast iron
- Common on large diameters, where cutting a sprocket out of solid bar would waste a great deal of metal and machining time. Casting gives a near-net shape, so a big sprocket becomes affordable. The trade is a longer pattern lead time and a minimum quantity that suits the tooling.
- Engineering plastic
- Used where quiet running, no lubrication and light weight matter more than load capacity — conveyor and packaging lines are full of them. A plastic sprocket will not rust and will not damage a chain if it fails, but it cannot take the load of a steel one, and it needs a chain that suits it. This is the same family of trade-offs that governs moulded plastic gears, where the material also has to be matched to the mating part rather than chosen alone.
One clarification saves arguments. "Stainless" describes the body of the sprocket and says nothing about its teeth. A stainless sprocket is usually supplied soft, because hardening stainless is a different and more expensive process, so stainless buys you corrosion resistance and gives up hardness. If you need both, say so — it is a different quote, not a different word.
Heat Treatment: What "Hardened" Does and Does Not Tell You
A chain roller is a hard piece of steel rolling over a tooth under load, so the tooth surface is a wear surface. A sprocket cut from soft steel will work, and it will wear its teeth into a hooked shape long before a hardened one does. This is why the single largest difference between two identical-looking sprocket quotes is almost always a sentence that does not appear on either.
Hardening, though, is a family of processes rather than one thing, and they do not give the same result:
- Through hardening
- The whole part is hardened and then tempered, so it is hard throughout. Simple to do and cheap, and it makes a tough sprocket that resists wear at the tooth. The trade is that a fully hard part is less forgiving of a shock load or a poor fit, because there is no softer core to absorb anything.
- Induction hardening
- Only the tooth region is heated and hardened, leaving the centre and the hub soft and tough. This gives the combination that most drives actually want: a hard wearing surface on the tooth with a shock-tolerant body underneath. It is more process control than through hardening, and it is what a careful supplier will offer when you ask how the teeth are hardened.
- Case hardening
- A hard skin is produced chemically, and how deep that skin goes is a process variable the supplier controls. This is where the word "hardened" becomes useless on its own, because a thin case and a deep case behave very differently in service, and both can honestly be described as hardened.
Three questions turn the word into a specification, and all three are cheap to ask before the order rather than after the failure:
- Which process, and how deep? Induction hardening with a stated depth is a specification. "Hardened teeth" is a claim. Ask for the hardness range and the depth in writing, and compare it between suppliers rather than comparing adjectives.
- Is the hardness tested, and is there a record? Hardness is measurable, so a supplier who hardens to a specification usually has a result to show. A supplier who cannot produce one has told you how much control they have.
- Is the bore finished before or after the heat treatment? This is the question buyers never ask and it decides whether the sprocket fits. Heat treatment moves metal: a bore finished before hardening can come out of the furnace slightly out of round or slightly different in size, and a sprocket that will not go on the shaft is scrap. The good answer is that the bore is finished after hardening, or that the bore is protected and checked afterwards.
There is one more consequence worth knowing. A hardened sprocket is much harder to modify than a soft one, so a hardened bore cannot be opened up on site with a hand tool. If there is any chance you will need to change the shaft fit, the bushing design described earlier earns its price exactly here — the bushing takes the change, and the hardened sprocket is left alone.
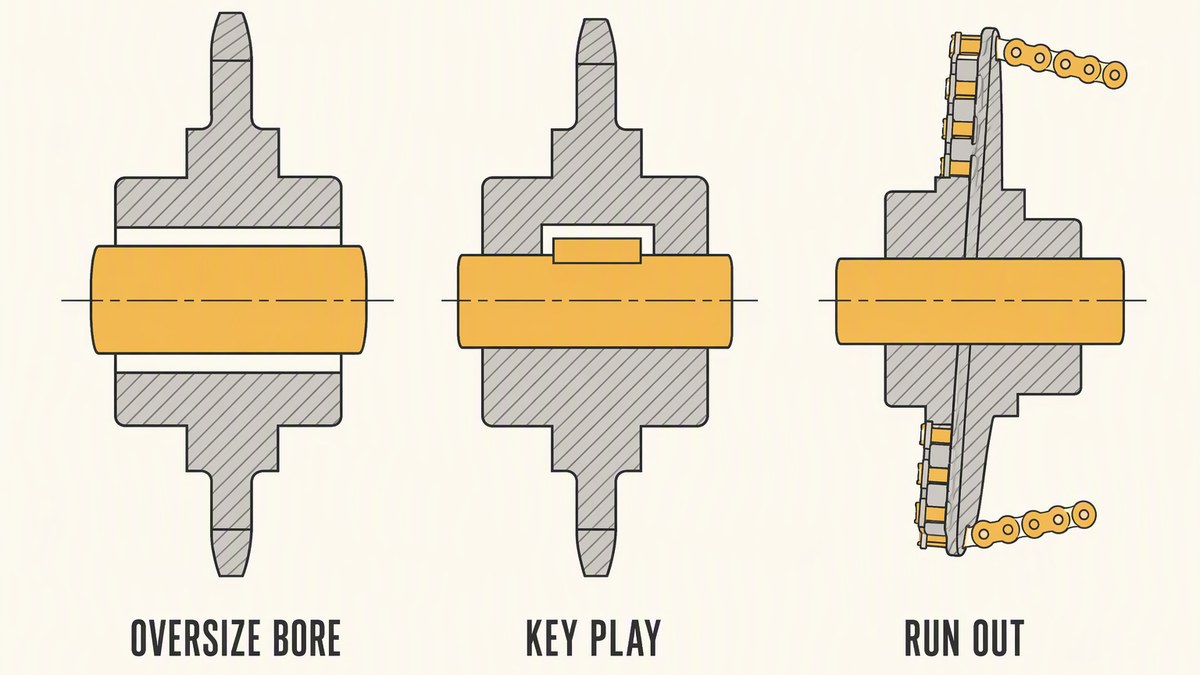
Bore, Keyway and Run-Out: the Fits That Decide Everything
A sprocket can be cut perfectly and still destroy a drive, because the fit between the sprocket and the shaft is where a good part becomes a bad installation. Three features carry that risk, and all three are settled on the drawing.
The bore. It has to match the actual shaft, not the shaft the machine was specified with. A bore that is too tight cannot be assembled without heat or force; a bore that is too loose lets the sprocket move, which is worse, because a sprocket that can slip eventually does. Because a bore cannot be shrunk, the safe habit is to measure the shaft before the order and to give the supplier the measurement rather than a nominal size.
The keyway and key. The key is deliberately the weakest part of the joint, so that a shock load shears a cheap key instead of twisting the shaft. That only works if the key is the right size for the shaft and the keyway is cut to match. A key that is too small becomes a permanent source of play; a key that is oversized stops being a fuse. The keyway position also matters more than it looks, because it decides where the set screws land relative to the load.
Run-out. A sprocket has to be concentric with its bore and square to the shaft face. If it is not, the chain tension goes tight, loose, tight as the sprocket turns, and a drive that runs like that destroys the chain and then blames the chain. Run-out is measurable, so it is a line on an inspection report rather than an opinion — and for a large sprocket it is the check most worth asking for, because a large part is where the error is largest.
Which Standard, and What the Drawing Has to Say
Standards matter on a sprocket because they describe the joint between the tooth and the chain, and that joint has to be identical on both sides. The American family of precision power transmission roller chains, their attachments and their sprocket teeth is covered by ANSI/ASME B29.1; other regions work to their own national and international equivalents, and the two families do not label their chains the same way.
The practical consequence is worth repeating in its own sentence: match the sprocket to the chain by pitch, roller diameter and tooth count, not by a part number alone. A number only means something inside the system that issued it, so a sprocket bought against a number from the wrong system is a mismatch that looks correct until the chain is offered up to it.
What a standard does not do is tell your supplier the four things only you know. A tooth profile standard says what the teeth should look like; it says nothing about how hard they are, what the bore is, how the part is mounted, or how much run-out is acceptable. Those live on your drawing, and a drawing that omits them has handed the decisions to whoever quotes lowest. A sprocket drawing should state, at minimum:
- The chain's pitch and roller diameter, and the system they are quoted in, or the chain's part number together with the standard it belongs to.
- The tooth count, and which sprocket in the drive it is.
- The material and the heat treatment, with a hardness range and depth rather than the word hardened.
- The bore, the keyway, the set screw or bushing arrangement, and the shaft measurement they were taken from.
- The hub style and the overall dimension that has to fit the space available.
- The acceptable run-out, and the marking that has to be stamped on the part so it can be identified in the store.
The tooling question sits on top of all of that, and it is the same question that governs every machined part. A sprocket cut from bar stock needs no tool at all, which suits small quantities; a cast or formed sprocket needs a pattern, which suits volume. Where the crossover falls depends on how much metal the part wastes and how much machining time it saves, and if you have priced that trade before, the arithmetic is set out in what an the tooling price on a sprocket — different process, identical question about when a tool pays for itself. Whichever route you take, settle who owns the pattern or the drawing before it is made, along the lines of tool ownership after a sprocket order, because a part you cannot re-quote is a part whose price you no longer control.
Chains and Sprockets Wear as a Pair
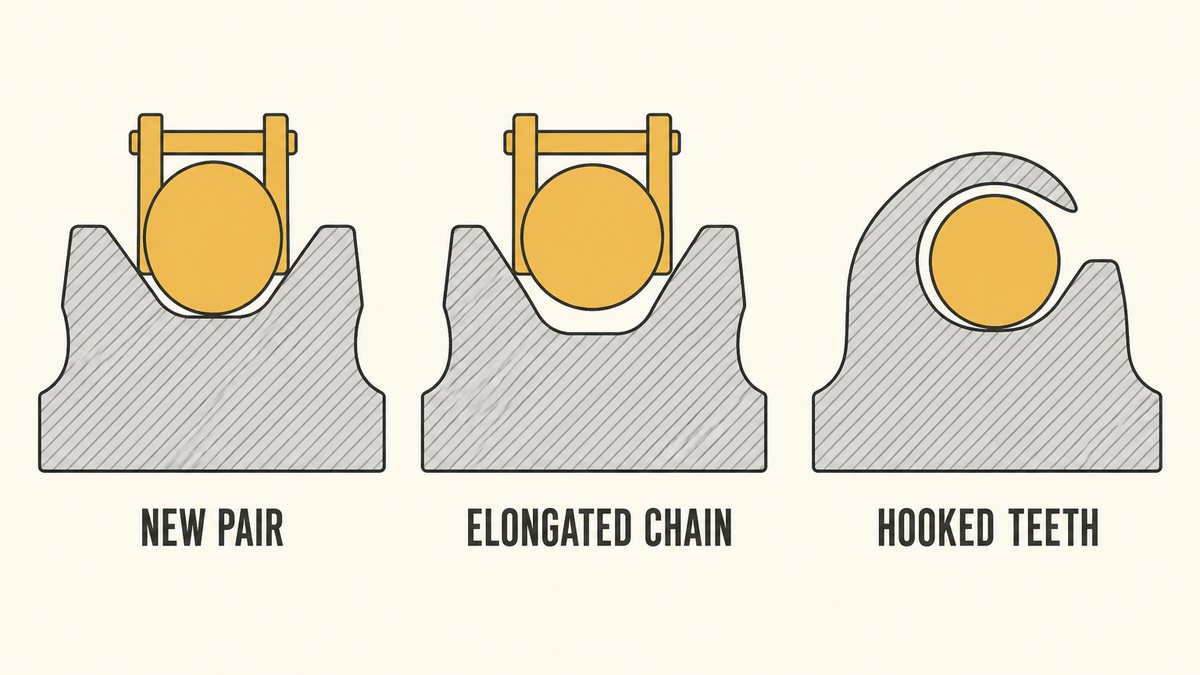
This is the single most expensive misunderstanding in chain drives, and it costs money in a way that looks like a saving. A chain does not wear by getting thinner; it wears at the pins and bushes, so the chain gets longer. Engineers call it elongation, and the effect is that the pitch of a worn chain is bigger than the pitch the sprocket was cut for.
Once the pitch has grown, the chain no longer sits down in the tooth seat. It rides higher, on the flanks of the teeth, and the load lands in the wrong place. Two failures follow from that, depending on which part you replaced:
The conclusion is not that you must always replace both. It is that you have to measure both, and that a chain should be replaced at a defined wear limit rather than when it breaks. Chain wear is measurable by comparing the distance over a set number of pitches against what it should be, and a drive with a stated limit is a drive that gets its chains changed on a schedule instead of after a breakdown.
One more habit extends the life of the pair more cheaply than any material upgrade: lubrication. A dry chain wears at the pins, elongates faster, and then takes the sprocket with it. The cheapest way to make a chain drive last is to keep it lubricated and correctly tensioned, and the cheapest way to waste a hardened sprocket is to run it dry.
Guarding: the Compliance Item Buyers Forget to Specify
A chain and sprocket drive is a nip point. Where the chain enters the sprocket, the gap between them closes, and that closing gap will take a finger, a sleeve or a loose glove. That is why mechanical power-transmission apparatus is regulated rather than left to engineering taste, and in the United States the rule that covers this equipment is 29 CFR 1910.219, the standard for mechanical power-transmission apparatus.
Why this belongs in a sourcing guide rather than only in a safety manual is that the guard is a constraint on the sprocket you order. A guard has to enclose the drive with clearance, so the space available decides how large the driven sprocket can be and which hub style fits underneath. Buy the drive first and the guard second, and you can easily end up with a sprocket that no standard guard will cover — at which point the choices are a bespoke guard, a redesign, or an unguarded drive that should not ship.
The habit worth adopting is to ask for the guard envelope as part of the drive specification. When the available height and width are known before the sprockets are chosen, the hub style and the tooth count are picked inside a real space instead of being adjusted afterwards. And if the machine is going into a regulated market, the guard is part of what has to be documented, so it is a deliverable rather than an afterthought.
Who Makes Sprockets, and What a Cheap Quote Leaves Out?
Sprockets are made by three very different kinds of supplier, and the difference shows up in what they can answer rather than in what they can quote.
- A power-transmission factory. Cuts teeth, hardens in house, and knows what pitch and roller diameter mean. It can tell you which hardening process it uses, because it runs the furnace.
- A general machine shop. Can cut a sprocket perfectly well and will send it out for hardening. Competent, but the heat treatment becomes a third party in your quality chain, and the process record is one step further away.
- A reseller. Quotes from a catalogue or from someone else's drawing. Fine for a standard stock part and hopeless for a drive with an unusual tooth count, because there is nobody in the conversation who understands the question.
A cheap quotation is usually a quotation for less than you assumed, and there are five places the scope shrinks:
- The heat treatment. A light case, or no treatment at all, is described as hardened. This is the difference that decides whether the part lasts one season or five, and it is invisible on delivery.
- The tooth profile. A low quote is often a formed or stamped tooth rather than a cut one, which is fine for a light conveyor and wrong for a loaded drive. The chain will tell you: an inexact profile wears the chain as well as itself.
- The order of boring and hardening. A bore finished before heat treatment can come out of the furnace distorted, and the sprocket will not go on the shaft. This is the most common form of "it does not fit" on a hardened sprocket.
- Run-out and dimensional checking. A quote with no inspection line is a quote with no inspection. Ask for a first-article report that includes the bore and the run-out, because those are the two numbers that decide whether the part works.
- Marking. A sprocket with no tooth count and no pitch stamped on it is a sprocket that will be misfiled in the store, and a misfiled sprocket eventually gets fitted to the wrong drive.
Two checks make the comparison cheap. First, establish who you are talking to, because a factory and a reseller answer a question about hardening processes completely differently — the method is described in checking whether the supplier makes the part. Second, check any certificate that carries weight against the issuer's own record rather than against a photograph, using the approach set out for looking the sprocket certificate up at the certifier. Then inspect what arrives against a stated plan rather than against a feeling, using a written how many sprocket units to pull per batch so that acceptable means the same thing to both sides.
Finally, price the part where it lands. A sprocket is dense steel, so it is heavy for its size and freight is charged on weight, which means the the landed total on a sprocket order. A slightly more expensive sprocket that arrives correct and hardened is usually the cheaper one.
What Are the Common Failure Modes?
Sprocket failures are easy to read once you know the signatures, and each one traces back to a decision rather than to bad luck. Five cover almost everything a buyer meets.
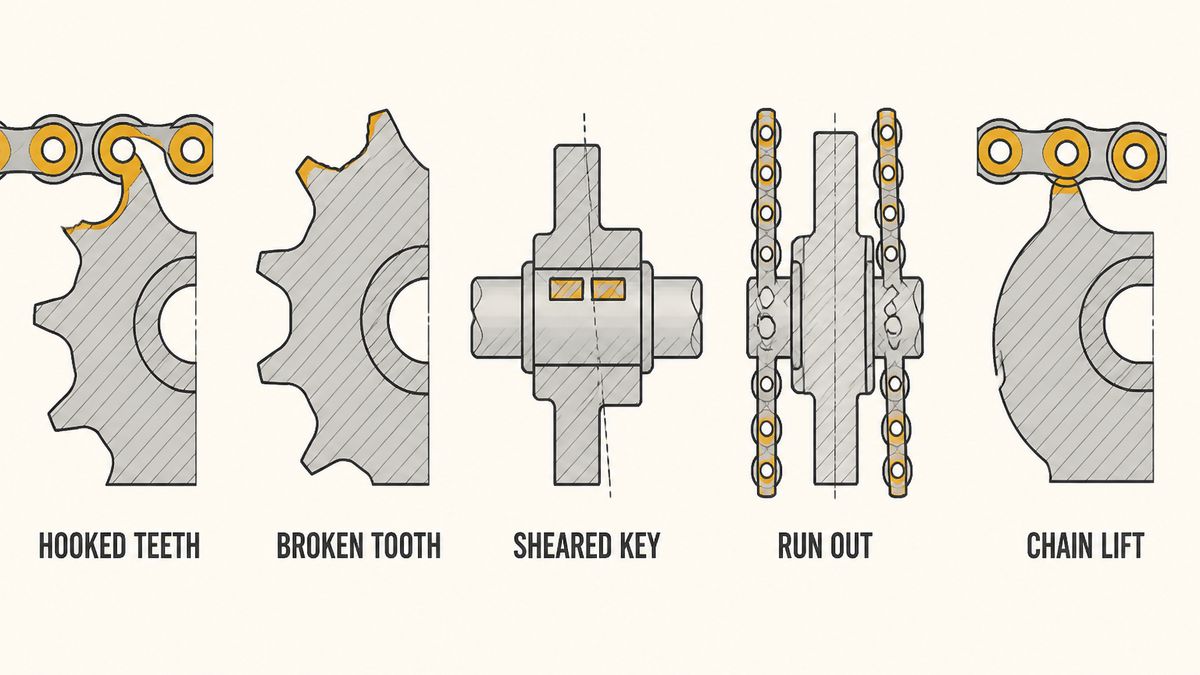
- Teeth worn into a hook
- The driving face of each tooth wears into a crescent that curves the wrong way, so the chain no longer sits down into the seat and starts riding on the flanks. It is a slow failure and the cheapest one to catch, because the hook is visible long before the drive stops working. A soft or lightly cased sprocket reaches it far sooner than a properly hardened one.
- A broken tooth
- Usually a shock load landing on a tooth that had nothing underneath it to absorb the energy, or a tooth hardened right through with no tough core. It is often blamed on the material when it is really a question about which hardening process was used.
- A sheared key with the sprocket turned on its shaft
- A bore that was slightly loose, or a key that was undersized, lets the sprocket rotate a little on every start. The movement works the key until it shears, and by then the bore and the shaft are both damaged. This is the failure that a bushed mounting prevents, because the bushing grips the shaft along its whole length rather than relying on one key.
- Run-out, or a sprocket that wobbles
- A sprocket that is not concentric with its bore, or not square to the shaft face, makes the chain tension cycle once per revolution. The drive then wears the chain and the tooth unevenly, and the damage looks random when it is not. It is measurable before the part ships and it is the check most worth asking for on a large sprocket.
- A chain that climbs and jumps the teeth
- An elongated chain or a slack tension lets the chain ride up the tooth instead of into the seat, and eventually a roller skips over a tooth entirely. It is regularly blamed on the sprocket, and just as regularly caused by a chain that should have been replaced at a measured wear limit long before.
Four of those five were settled by the specification and one by the maintenance schedule, which is the argument for spending the time on the hardening, the bore and the run-out rather than on the last few per cent of the unit price.
Frequently Asked Questions
How do I match a sprocket to a chain?
Match on three dimensions rather than on a part number: the chain pitch, the roller diameter and the tooth count. Those describe the joint between the chain and the sprocket and decide whether the two mesh at all. The American and the European chain systems describe similar chains but label them differently, so a number only means something inside the system that issued it. If you are unsure, send the chain's part number together with the standard it belongs to, and ask the supplier to confirm the pitch and roller diameter in writing before the sprocket is cut.
Why does the small sprocket wear out first?
Because fewer teeth are in mesh at any moment, so each tooth carries a larger share of the load, and because each chain link has to flex through a bigger angle as it enters and leaves a small sprocket. The driver is normally the small one, which is why it is the first part of a drive to fail. The practical response is to put the better hardening on the small sprocket rather than on both, since hardening a small part costs far less than hardening a large one.
Do I need hardened teeth on both sprockets?
Not necessarily, and the money is better spent at the driver. The small sprocket sees the most articulation and the highest load per tooth, so hardening there buys the most life for the least cost. The driven sprocket turns more slowly with more teeth in mesh and wears less. What matters more than hardening both is that the two sprockets and the chain are treated as one set, because a hard part running against a soft one wears the soft one out faster than either would wear alone.
Should I replace the chain and the sprockets at the same time?
Not always, but you have to measure both to decide. A chain gets longer as it wears, so a worn chain rides high on the tooth flanks and can damage a new sprocket quickly, while a new chain on a hooked sprocket wears out early and gets blamed for it. Measure the chain wear against its stated limit and look at the tooth profile. If the chain is near its limit and the teeth are visibly hooked, replace both; if one is clearly good, replacing only the worn part is a reasonable decision made on evidence.
Can I re-bore a sprocket to fit a different shaft?
Only if it is not hardened in the bore, and only in one direction. A bore can be opened up but never reduced, so a change to a smaller shaft means a new sprocket. On a hardened sprocket the bore usually cannot be machined on site at all. This is exactly why a bushed sprocket is worth the small price difference: the bushing carries the shaft fit, so changing shafts costs you a bushing instead of a sprocket.
What is a taper lock bushing, and when is it worth it?
It is a separate part that grips the shaft and is drawn into a matching taper in the sprocket, so the sprocket is held by friction along the whole length of the bushing rather than by one key. It is worth specifying whenever the shaft size might change, whenever the drive will be maintained, and whenever the sprocket is hardened and therefore cannot be re-bored later. The trade is one more part to stock and one more thing to tighten correctly, which is small compared with a sprocket that cannot be adjusted.
Send the chain, not just the sprocket size
Tell us the chain pitch and roller diameter and which system they are quoted in, the tooth count and which sprocket in the drive it is, your measured shaft size, the load and duty, and whether the drive will ever be guarded or modified. Those answers settle the tooth profile, the material, the hardening and the bore before a price means anything. We will come back with the configuration we recommend and why, the material and the hardening process named with a hardness range and depth, the bore and keyway taken from your measurement rather than the size written on a drawing, the run-out we will hold, and a first-article report before the run is released — with the heat treatment and inspection lines shown separately rather than folded into the unit price.
Request a Sprocket Sourcing Quote
Questions & Comments
We read every one and reply within 24 hoursIf you are holding a sprocket quotation and trying to work out whether two quotes describe the same part, post three things and we can usually say: the chain pitch and roller diameter and which system they are quoted in, the tooth count, and your measured shaft size. If you already have drawings, add how the teeth are hardened and whether the bore was finished before or after the heat treatment. Those two lines explain most of the gap between two sprocket quotations, and they are the two lines a short quote tends to leave out.